For our full range of products and services, choose the relevant catalogue.
GREEN SAND · NO-BAKE · SHELL MOLD
Sand casting covers the widest size range of any casting process at the lowest tooling cost. A new mold is made for every casting, so the pattern is the main tooling cost and part size is limited mainly by mold and pour capacity.
Sand castings in steel, stainless, ductile iron and wear-resistant irons, from 0.2 to 110,000 lb (0.1 to 50,000 kg), cast through our foundry network and supported in the US.
This page compares green sand, no-bake and shell mold casting, lists the alloys and parts cast most often, and sets out how a sand casting project runs from drawing to delivery.
US office · 550 Albion Ave, Ste 230, Schaumburg, IL 60193 · +1 708 433 4160
Sand Casting for Steel, Stainless and Ductile Iron Parts
Sand molds take complex shapes, internal cores and varying wall sections that would be costly to machine from solid, and the same process covers a one-off replacement part and a repeat production program. The three sand processes differ in the mold: how it is bonded, how large it can be, and the finish it leaves on the casting.
As a sand casting supplier, Kormax matches each part to the foundry best suited to its size, alloy and volume, and manages the job from drawing review to delivery through a single point of contact.
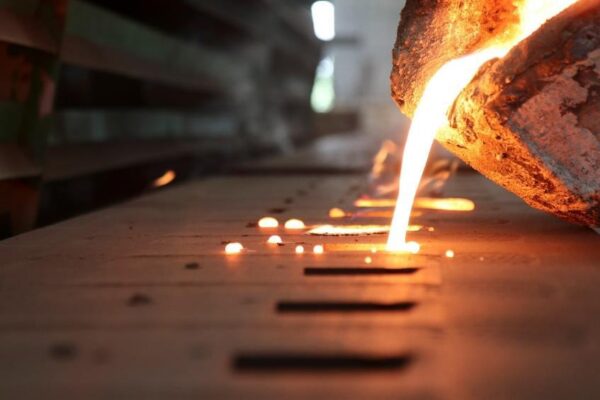
Green Sand Casting
1 – 165 lb (0.5 – 75 kg)
Moist, clay-bonded sand molds. Low tooling cost and fast mold preparation make green sand the economical choice for repeat production in ferrous and non-ferrous alloys.
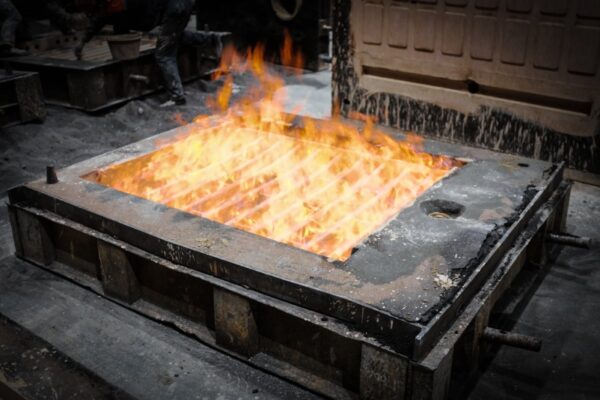
No-Bake Sand Casting
100 lb (45 kg) to over 110,000 lb (50,000 kg)
Chemically bonded sand cures at room temperature into a rigid mold that holds its shape for large, heavy-section components. Low-cost tooling suits low to medium volumes.
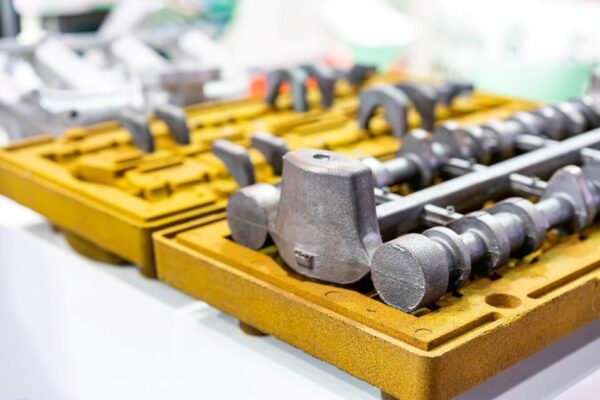
Shell Mold Casting
0.2 – 220 lb (0.1 – 100 kg)
Resin-coated sand cured against a heated metal pattern gives a very good as-cast finish and close part-to-part repeatability, which reduces machining on production runs. The metal pattern costs more up front, so shell mold pays back at medium to high volumes.
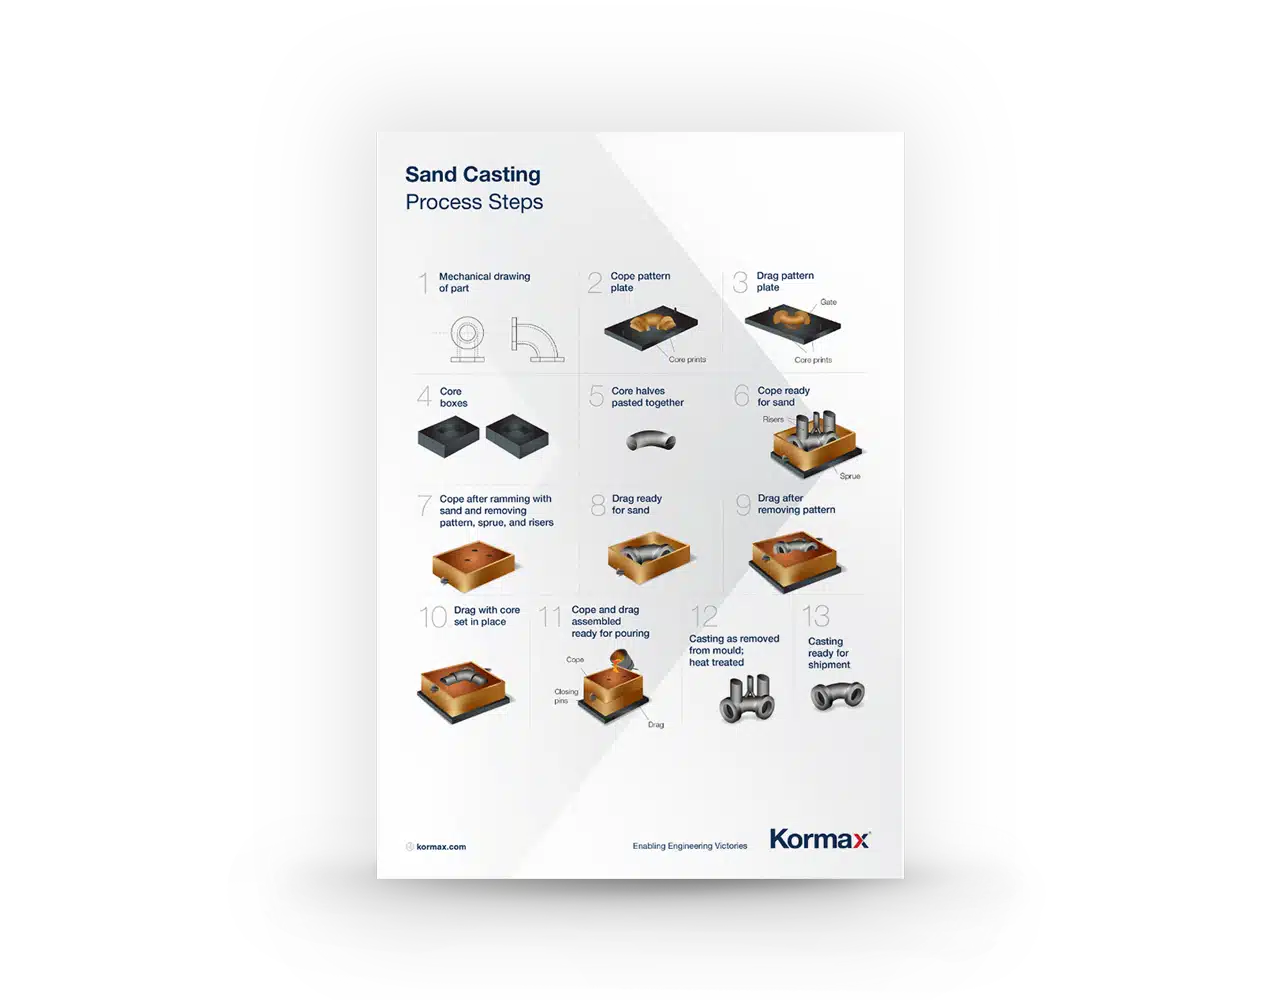
Sand Casting Process Steps
The foundry process from pattern to finished casting, as a one-page diagram.
Green Sand, No-Bake and Shell Mold Compared
The table compares the three sand processes on the factors that usually decide the choice. Final selection depends on the drawing, the alloy and the annual volume.
| Green Sand | No-Bake | Shell Mold | |
|---|---|---|---|
| Part weight | 1 – 165 lb (0.5 – 75 kg) | 100 – 110,000+ lb (45 – 50,000+ kg) | 0.2 – 220 lb (0.1 – 100 kg) |
| Tooling cost | Low | Low | Medium |
| Design freedom | Average | Average | Good |
| Casting soundness | Depends on design and gating | Depends on design and gating | Average |
| Surface finish | Medium | Average | Very Good |
| Best for | Repeat production | Large, heavy sections | Small precision parts in volume |
| Development time | 4 weeks + | 4 weeks + | 4 weeks + |
| Production time | 3 – 8 weeks | 3 – 8 weeks | 3 – 8 weeks |
Green sand and no-bake keep tooling cost low across the widest weight range, and no-bake takes over where a part is too large or too heavy in section for a green sand mold. Shell mold costs more to tool and recovers it on small parts in volume, through a finer as-cast finish and less machining.
Sand Casting Alloys: Steel, Stainless, Ductile Iron and Wear Irons
The alloy follows from what limits the part’s life in service: load, corrosion, wear or heat. Kormax metallurgists review every enquiry for alloy and process fit before it is quoted, and castings in each family draw on our foundry network.
| Alloy family | Typical grades | Related markets |
|---|---|---|
| Carbon, Low-Alloy and Alloy Steel | ASTM A216 WCB; ASTM A148 Gr 105-85 | Construction, Transmission, Fasteners |
| Austenitic, Martensitic and Duplex Stainless Steel | CF8M, CF3M; martensitic and duplex grades to specification | Marine, Pump and Valve, Hydraulic Components |
| Ductile and Gray Iron | ASTM A536 ductile iron; ASTM A48 Class 30 – 40 gray iron | Automotive, Pipe Fittings, Valves, Hydraulic Components, Bearings |
| Wear Irons | Ni-Hard and high-chromium white irons; Ni-Resist | Mining, Crushing, Aggregate Processing, Cement, Pump Parts |
Composition and mechanical properties for each grade are on the casting alloys pages.
What We Sand Cast, and Who For
These are the parts sand cast most often, with the grades they are cast in and the industries that specify them. Sand casting takes the largest parts and heaviest sections; a part outside this list is often still in range, and the drawing settles it.
Pumps, Valves & Fluid Power
Pump casings, volutes and manifold blocks in thick wall sections, plus impellers, wear plates, back covers and valve bodies, for pump and valve OEMs and hydraulic equipment builders. Cast in ductile iron, carbon steel to ASTM A216 WCB, and CF8M and CF3M stainless, then machined, pressure-tested and finished to drawing.
Water & Wastewater Equipment
Large pump volutes, aeration and screen frames, and gearbox and drive housings at full equipment size, plus impellers and valve and hydrant bodies, for municipal and industrial water equipment OEMs. Corrosion-resistant stainless for wetted parts; ductile iron for housings and covers.
Mining, Quarrying & Aggregate
The heaviest wear parts: crusher bodies, mantles and bowl liners, jaw and cheek plates, mill liners, pump wet ends, and chute and feeder components. Manganese steel to ASTM A128, white and Ni-hard irons, and high-chrome grades where abrasion, not load, sets part life.
Off-Highway & Construction
Structural castings for earthmoving and forestry machinery: pivot and linkage housings, axle cases, cylinder end caps, transmission components and counterweights. Ductile iron and low-alloy steel to ASTM A148 Gr 105-85, cast and machined to the build schedule.
Oil, Gas & Power Generation
Pressure-containing bodies in heavy wall sections: valve and pump bodies, compressor and turbine housings, and heat exchanger components. Carbon steel to ASTM A216 WCB, low-alloy grades for elevated temperature, and duplex and super-duplex stainless for sour and produced-water service.
Machine Shops & Industrial OEMs
Contract machine shops and industrial equipment builders source sand castings through Kormax to keep their machining capacity full: rail, material handling, compressor, gearbox and general industrial components, from one-off prototypes to repeat production. Supplied raw for finishing or machined to print.
How a Sand Casting Project Runs with Kormax
A sand casting project runs in six stages, and the sample approved at stage three is the part delivered in production. The foundry process itself, from pattern to shakeout, is set out in the sand casting process steps.
- 01
Drawing Review
The drawing, specification and annual volume are reviewed by Kormax metallurgists for alloy and process fit, and the sand process is recommended on finished-part cost.
- 02
Methoding and Pattern
Gating, risering and cores are designed for the part, with MAGMASOFT® casting simulation where the part needs it, before the pattern is made. See casting design.
- 03
Samples and First Article
Sample castings are poured and inspected against the drawing, with material certificates, and production starts once the sample is approved.
- 04
Production
Molding, pouring, shakeout, fettling and heat treatment to the specification, under a PPAP and quality-control process.
- 05
Machining and Inspection
Castings are supplied raw or machined to print, then inspected. Independent third-party inspection is standard, and material certificates and inspection reports ship with every order.
- 06
Delivery and Supply
Freight to the agreed dates, with consignment and buffer stock or scheduled supply for repeat parts.
Why Buyers Choose Kormax for Sand Casting
Kormax manages the supply chain between the drawing and the delivered casting. Four points set out how.

Foundry Network
Each part is matched to the foundry best suited to its size, alloy and volume, and repeat parts can be dual-sourced where supply security matters.

Single Point of Contact
Tooling, samples, production, machining, inspection and freight are managed as one job, so one sand casting company answers for the finished part.

Supply Security
Consignment and buffer stock, scheduled supply programs and dual-sourced foundries keep repeat parts moving when one source is disrupted.

Competitive Tendering
Parts are tendered across the foundry network, with low-cost tooling options and no hidden surcharges.
Kormax operates a management system certified to ISO 9001, ISO 14001 and ISO 45001.
Sand Casting FAQs
Tooling cost depends mainly on the pattern: its size, the number of cores, and whether it is made in wood, resin or metal. Green sand and no-bake patterns are typically the lowest-cost tooling of any casting process; shell mold needs a heated metal pattern, which costs more and pays back at medium to high volumes. Tooling is quoted for each part from the drawing.
There is no fixed minimum. Low pattern cost makes sand casting suit one-off prototypes and replacement parts as well as repeat production, and the process is recommended on the volume as well as the part.
No-bake sand casting takes single pieces over 110,000 lb (50,000 kg). Green sand covers 1 to 165 lb (0.5 to 75 kg) and shell mold 0.2 to 220 lb (0.1 to 100 kg). Each part is matched to the foundry with the mold and pour capacity for its size.
Sand castings have a rougher as-cast surface and wider dimensional tolerances than investment castings, and need draft and a machining allowance on critical faces. Where fine detail or finish decides the part, investment casting is usually the better route, up to 330 lb (150 kg).
Yes. Sand castings are supplied raw for finishing or machined to print, then inspected before shipping. Kormax machines only the castings it supplies.
Inspection is set by the specification and can include visual and dimensional inspection, ultrasonic, radiographic, magnetic particle and dye penetrant testing, chemical analysis, and tensile, impact and hardness testing. Independent third-party inspection is standard, and material certificates and inspection reports ship with every order.
Pattern development typically takes 4 weeks or more, and production 3 to 8 weeks, depending on part size, complexity and volume. Lead times for each part are confirmed at quotation.
Request a Quote
Kormax supplies sand castings in steel, stainless, ductile iron and wear-resistant irons to order for the US. Send the drawing or 3D model, the alloy and the annual volume to request a quote.