Buying metal castings is not always straightforward. No matter your knowledge base, there is a lot to understand – on both your end and the foundry’s. Factors like alloy selection, molding/finishing processes, core requirements, supply terms… to get the most value for your money, all of these need to be understood. But by simply expanding on your knowledge of metal casting, well, you will have already started the process of evaluating costs and benefits. Before we gear up for the more well-known costs of metal casting, there are a few considerations you may not have thought about.
Economies of Scale – Weigh it Up
Let us say you have a casting order requirement that’s less than 220 lb (100 kg), but the foundry you are currently working with accommodates medium- to large-scale casting. You will be wasting crucial capital on both their furnace’s power and casting yield. It is essential to ensure that the foundry you have chosen is right for your requirements. For example, for order volumes over 2,200 lb (1 metric ton) you should choose a foundry geared for medium and high economies of scale, ideally with a furnace of 1,100 lb (500 kg) or larger.
Foundry Alterations – Be Prepared
When negotiating the purchase of castings from any foundry, do not expect your product to be supplied at cost. If your foundry goes out of business, you are likely to face a large expense from new patterns at a new foundry, or at least from modifying existing patterns to suit another foundry’s molding equipment. Make sure to choose a foundry that will remain in business for as long as you will be requiring your castings, so be realistic on price when choosing a foundry.
Local Scrap and Supply Chain – Check for Kinks
So much of your foundry’s raw material cost will be down to supply chain and local scrap availability. It is important to identify not only what your chosen foundry’s costs are during the casting process but also what costs might be included before anything has even touched the furnace. Read on to find more about material costs below.
The Metal
To calculate the cost of metal you need to know three things: alloy type, casting weight, and total tree weight (including runners and risers). Alloys are a combination of a base metal like iron, copper, or aluminum, all in conjunction with a range of additives. These additives can cause huge changes to the properties of metal even in very small amounts. When the correct, specific alloy or composition is determined, the casting process will begin to take shape.
The Foundry
Your foundry will calculate the correct amount of base metal required per lb (kg) of casting and the quantity of alloying elements required to achieve the desired composition. But take note, in some cases a higher amount of additive is required to allow for melting loss and oxidation, depending on your casting process.
Once the amounts of base metal and alloy additives have been determined, the source of the metal should be selected to achieve the lowest cost of raw materials. Global metal exchanges such as the London Metal Exchange (LME) are often used as cost benchmarks, and are a great way to analyze the costs of the raw materials you need.
LME Prices, USD (5 October 2026)
Base metal prices move daily. The figures below are London Metal Exchange (LME) official cash settlement prices on 5 October 2026, shown as a reference point rather than a quote.
| LME contract | USD per lb | USD per metric ton |
| Steel Scrap CFR India (Fe)* | $0.18 | $407 |
| Aluminum (Al) | $1.41 | $3,107 |
| Copper (Cu) | $6.55 | $14,430 |
| Nickel (Ni) | $7.02 | $15,470 |
| Tin (Sn) | $24.61 | $54,250 |
| Zinc (Zn) | $1.71 | $3,774 |
| Lead (Pb) | $0.83 | $1,830 |
Source: London Metal Exchange, official cash settlement prices, 5 October 2026. *Steel scrap: LME Steel Scrap CFR India (Platts), month-two closing price. Current prices are published at lme.com.
Now you have your materials, let us break down your foundry’s furnace.
The first processing of metal is the melting process, which is performed in your foundry’s furnaces. Induction furnaces are the most common type for production casting; cupola furnaces are still used for cast iron.
But, as always, there are costs.
The main cost of metal melting is electricity. But operational labor and maintenance have a significant impact too. Most foundries know how these costs translate to their metal melting cost per lb (or per kg) at spout – it is the average cost for them to get 1 lb (or 1 kg) of any molten metal prepared for pouring from the furnace. But with varying foundries come varying workforce sizes and power needs, so be sure to take these into account.
Alloy also drives melting cost: alloys with a higher melting point need more energy and furnace time per lb. That said, a highly efficient foundry can achieve a melting cost as low as $0.14 USD per lb ($0.30 per kg) for cast iron, whereas low-volume furnaces with expensive electricity can cost as much as $0.68 USD per lb ($1.50 per kg). The melting cost then needs to be multiplied by the casting weight and divided by the casting yield. The yield is the percentage of the casting tree that is the actual casting. This is where choosing a foundry that works at the right scale comes into play. Remember – bigger is not always better, as furnace melting cost is regulated in part by the kilowatt capacity and efficiency of the furnace. So, what type of costs can you expect to face when it comes to types of casting?
Molding Costs
Molding costs vary substantially depending on your favored process. From low to high – die casting, green sand casting, hard sand or resin sand molding, and then shell mold and investment casting.
Let us break them down.
Die Casting – Low material usage with a high output to labor cost ratio.
While the low cost of this process is a relief on expenditure, the geometry possible with this production process is limited and the tooling cost is high. That said, the molding cost of this production process is normally a small fraction of the metal cost going in.
Green Sand Molding – Relatively low cost due to reuse potential of sand and output per labor hour being high.
This is made achievable with the common semi-automatic jolt-squeeze molding machines and less common fully automated molding machines. Using a semi-automatic molding machine producing small molding boxes of 24 × 16 in (600 × 400 mm), a molder could typically produce 8–15 molds per hour. As molds become more complicated or larger, the output slows as molders need to insert cores and take more care to ensure forming of detailed impressions. For a small molding box, the factory cost allowance would be about $0.50 USD per box plus the allocation of labor.
Hard Sand Molding – Reasonable cost due to sand reclaiming technology
Includes sodium silicate sand and furan resin sand casting. Furan no-bake molds mix silica sand with roughly 0.8–1.2% resin, cured by an acid catalyst. Sodium silicate molds use a silicate binder hardened by CO2 gas or an ester. Both typically cost about twice as much per mold as green sand, depending on the binder, mixer output and molding rate.
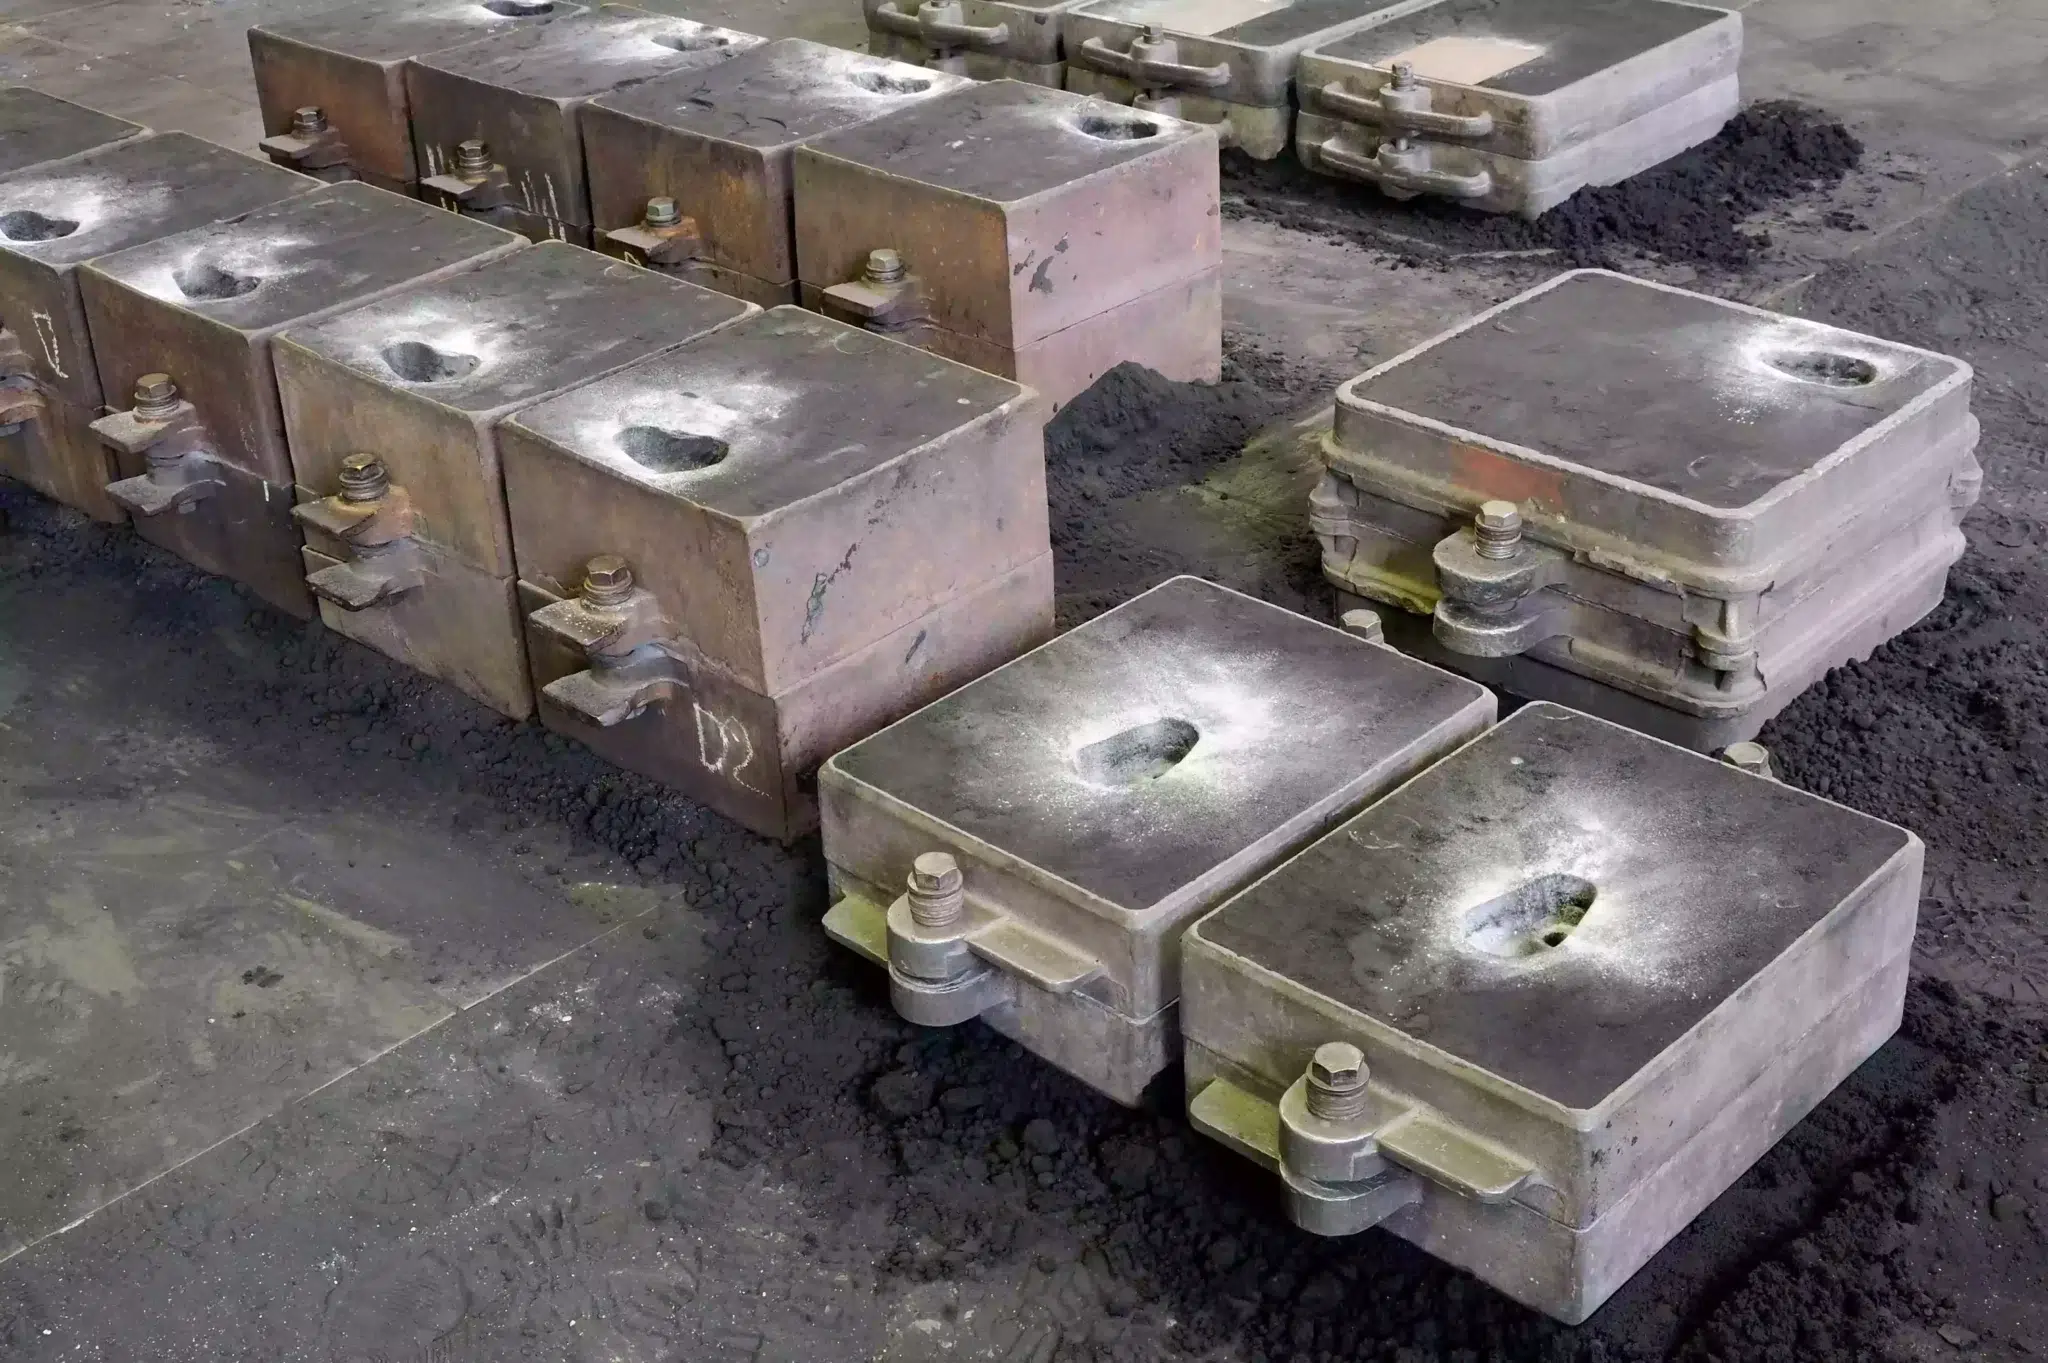
Shell Mold Casting – Higher cost, driven by resin-coated sand that costs more to buy and is harder to reclaim than green sand.
For a small mold, 20 × 20 in (500 × 500 mm), a shell mold can easily cost between $10–15 USD per mold. The advantage, however, is that this molding process achieves the best surface finish and level of detail of any sand casting process.
Lost Wax (Investment) Process – High cost, offset by reduced finishing and machining.
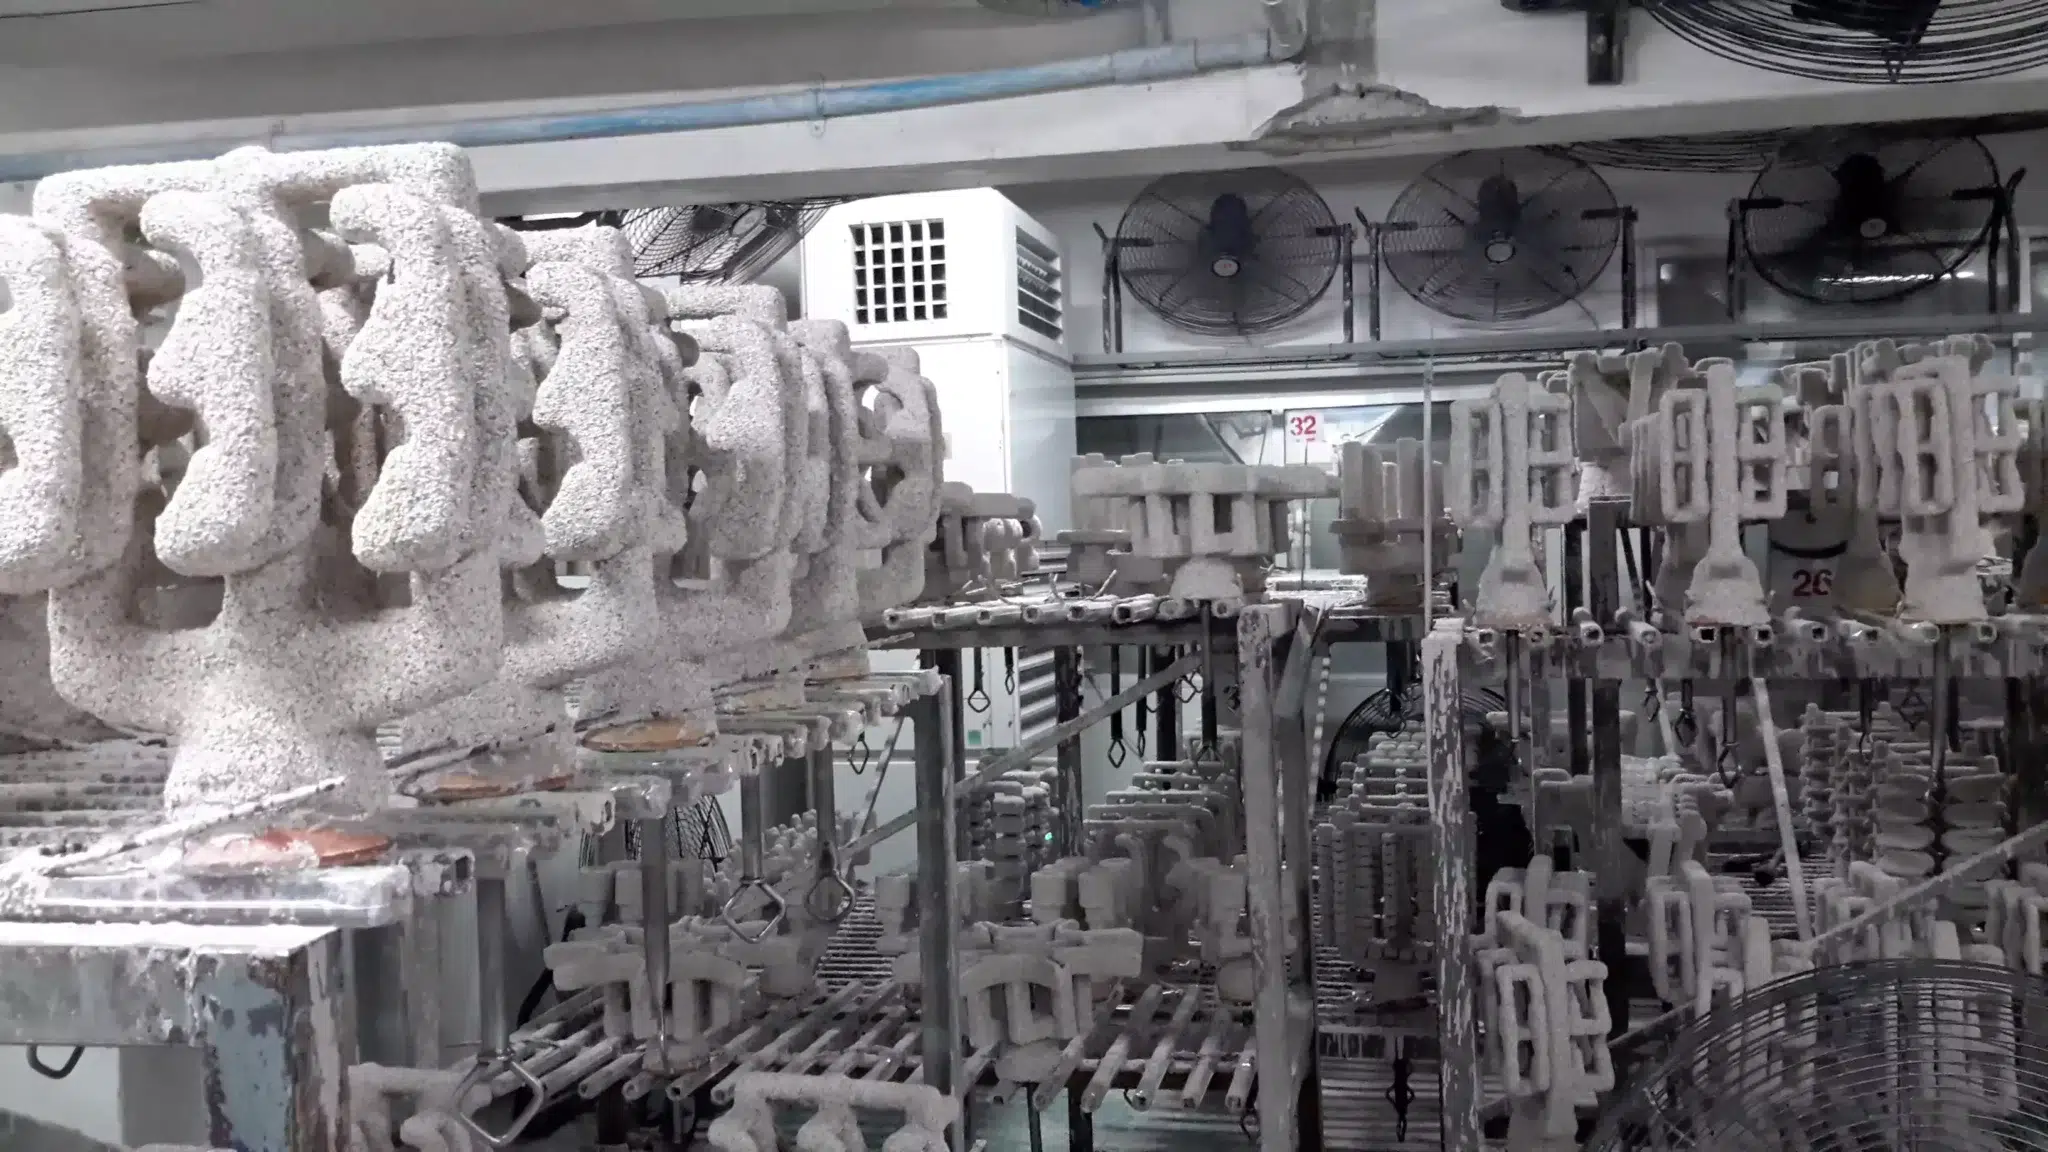
There is the initial wax injection process, the wax assembly, followed by multiple coatings, then the final de-waxing process, making it a labor-intensive method. The cost of each step of this process is relative to the level of efficiency and automation, and the cost of labor. This means the cost can vary substantially from one foundry to another. The advantage of eliminating finishing work and machining costs comes from an as-cast surface finish of around 125 µin Ra (3.2 µm Ra) and linear tolerances of typically ±0.005 in per in (±0.13 mm per 25 mm), depending on part size and alloy.
A sidenote on molding – cores are often used to achieve internal cavities. They are formed using sand, normally using the shell mold casting process or hard sand process depending on the preciseness of detail required!
Finishing Costs
Shot Blasting – This is done after the castings are poured and knocked out of their mold to clean up the casting and remove sand particles. The cost of shot blasting would normally only be 2–5 cents per lb (5–10 cents per kg) of casting.
Fettling – Removing gates, risers, flash and burrs after the casting is knocked out of the mold. This is a labor-intensive process and particularly required for castings produced by green sand molding and hard sand molding. The time requirement ranges depending on the complexity and size of the casting. A simple casting that weighs 11 lb (5 kg) would typically take 0.5–1 minute of fettling, whereas a complex casting weighing 220 lb (100 kg) could take 20–30 minutes or more.
Machining Cost – Usually the most expensive finishing process. Machining cost is dependent on the number of set-ups, the time required per process, cost of the machine, cost of cutting tools, cost of labor and volume. With this number of variables, we cannot give any suggested rule-of-thumb costs here. For sand castings where the machining cost is high, we would suggest considering if the lost-wax molding process would allow you to save more effectively. The lost-wax process can achieve complex geometries with a smooth, accurate surface finish that often reduces machining time or removes it entirely.
Other Finishing Processes – Painting, laser etching, polishing and plating. The costs for all these processes are dependent on the volume, quality requirement, level of automation and the cost of labor. When these processes are required, the costs are normally only a small percentage of the overall cost.
Before we conclude, however –
Supply Terms
Supply terms are a critical cost that many firms fail to consider when assessing costs. Supply terms set who pays freight and when payment falls due, which determines the freight cost incurred getting your castings delivered and the cost of capital if you need to pay for your castings ahead of when they are required.
Remember to consider the Incoterms in any foundry’s quote. If EXW (Ex Works) or FOB, then ensure you get a freight quote and add an administrative factor to cover the cost of you needing to arrange the inwards freight.
Remember to factor in the cost of capital. This is the time from when you need to pay for the castings to when you actually need the castings. If the foundry stipulates high minimum order quantities and is based far away, then the time between when you pay for your castings and when they are finally used may be significant. Apply your own cost-of-capital rate to this period to ensure you are factoring this in.
Conclusion
In any case, as times change, and the market fluctuates, what processes, materials, and foundries you value will do too. But one thing will always stay the same – knowledge is the most valuable tool at your disposal.
Keep yourself informed so that you can cut down costs and balance quality and value.
Kormax supplies sand and investment castings to order for the US. Send your drawing, alloy and annual volume to request a quote.